Engineering Reliability: How Laser Surface Preparation is Securing the Critical Joints of Lightweight Structures
In the high-stakes world of lightweight structural manufacturing—whether for next-generation bicycle frames, drone chassis, or aerospace components—performance is not defined by design alone. While CAD optimization and Finite Element Analysis (FEA) play an essential role in theory, long-term reliability is determined on the shop floor, at the precise point where materials are joined.
For manufacturers producing high-value lightweight structures, welding consistency has become the decisive factor in safety and performance. Increasingly, engineers in the Space Coast's thriving manufacturing sector are finding that welding quality is not just a function of current and voltage, but of the microscopic surface conditions present before the arc is ever struck.
The Manufacturing Reality Behind High-Value Alloys
Industries producing premium lightweight structures face a common engineering challenge: achieving the optimal balance between mass reduction and structural integrity. Titanium and aluminum alloys offer clear advantages for this strength-to-weight ratio, but they are notoriously unforgiving during fabrication.
These materials are highly sensitive. Surface contamination, naturally occurring oxidation, and even invisible handling residues can significantly affect weld behavior. In critical applications, such as an airframe bracket or a high-performance bicycle head tube, welding consistency directly influences structural safety, fatigue resistance, and overall product reliability.
Small variations at the joint level can have amplified effects. A microscopic inclusion today can become a stress fracture after 10,000 load cycles.
Hidden Risks in Conventional Workflows
For engineers and quality managers, the impact of trace contamination is often the "ghost" in the machine. In titanium welding, for instance, even a faint oil film can introduce hydrogen into the weld pool, leading to embrittlement that isn't detected until destructive testing.
This leads to a frustrating pattern where identical welding parameters produce different results from one batch to the next. Manufacturers often chase their tails adjusting voltage or wire speed, when the root cause lies in the inconsistent surface condition prepared by manual abrasion or chemical wiping.
Furthermore, traditional methods often necessitate rework. Post-weld grinding or reinforcement adds weight and alters the engineered stress distribution of the part—compromising the very benefits that lightweight design is meant to deliver.
The Q1 Solution: Stabilizing the Weld Pool
Welding quality is the outcome of a system, not a single step. Surface condition determines how heat flows, how the molten pool behaves, and how the joint solidifies. By addressing surface cleanliness upstream, manufacturers stabilize welding outcomes at their source rather than compensating after the fact.
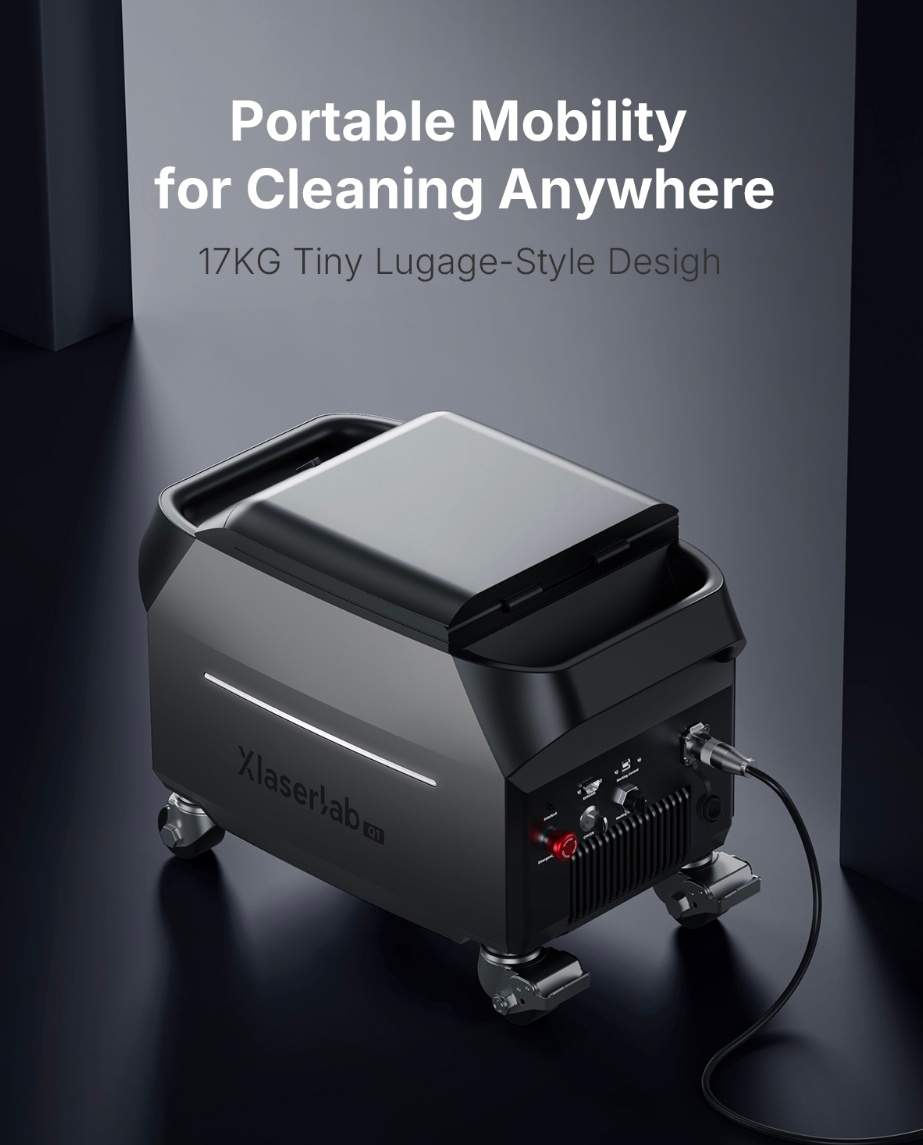
This shift toward proactive process control is driving the adoption of solutions based on xlaserlab laser surface cleaning. The Xlaserlab Q1 is being integrated into manufacturing lines as a dedicated pre-weld treatment method, replacing variable manual processes with a repeatable, digital standard.
The Q1 enables non-contact surface preparation specifically tuned for titanium and aluminum alloys. By selectively removing oil films and oxides without damaging the base material, the process preserves the substrate's integrity. Unlike wire brushing, which can leave conductive debris (FOD), or chemical cleaning which can leave residue, the laser provides a chemically pure surface.
As a dependable fiber laser cleaning machine, the Q1 delivers controlled, repeatable surface treatment. This is an essential requirement for multi-batch production where consistency defines engineering quality. Rather than adjusting welding parameters to accommodate surface variation, manufacturers establish a predictable baseline before welding begins.
Practical Applications in Structural Manufacturing
The integration of laser surface preparation is reshaping how critical components are fabricated.
Pre-Weld Preparation of Lightweight Frames For tubular structures like bicycle frames or roll cages, laser surface cleaning ensures uniform joint conditions. This supports consistent bead formation and penetration, critical for meeting fatigue life requirements without over-welding.
Batch Production with Controlled Variability In serial manufacturing, process capability (Cpk) is king. Standardized laser treatment reduces the variability between batches, helping maintain consistent structural performance as production volumes scale from prototype to full manufacturing.
High-Performance Engineering Projects For applications where failure is not an option, such as aerospace ground support equipment or marine hardware, controlled pre-weld preparation supports more predictable long-term behavior and simplifies the Non-Destructive Testing (NDT) phase.
Tangible Benefits for Manufacturers
By integrating laser-based pre-weld surface preparation, manufacturers can achieve measurable engineering improvements. These include significantly improved welding consistency and more stable structural performance across production runs.
Crucially, it allows for the preservation of lightweight design intent. By eliminating the need for excessive safety margins or reinforcement welds to compensate for potential defects, engineers can keep products as light and efficient as originally designed.
Conclusion
Lightweight manufacturing is increasingly shifting from design-driven optimization to process-driven reliability. As materials approach their performance limits, control over fabrication variables becomes a competitive advantage.
Laser surface cleaning aligns with this evolution by addressing a critical, often underestimated process step. Within high-value engineering workflows, the Xlaserlab Q1 illustrates how controlled surface preparation can underpin welding consistency, structural integrity, and long-term performance.

